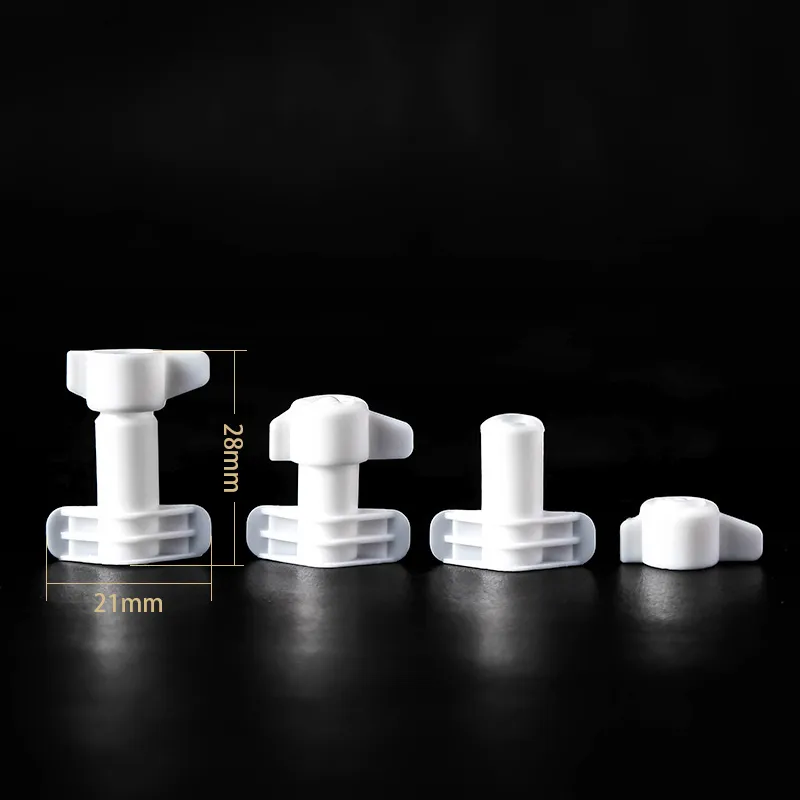
Coffee valves allow roasted coffee to release CO₂ while helping limit unwanted air from entering the package. The main difference between a stick-on coffee valve and a built-in coffee valve is how the valve is integrated into the coffee bag.
That difference affects installation, failure points, production workflow, and quality control. For buyers, the right choice depends less on the appearance of the valve and more on the bag structure, production process, and required level of integration.
What Is a Stick-On Coffee Valve vs a Built-In Coffee Valve?
How a Stick-On Coffee Valve Works
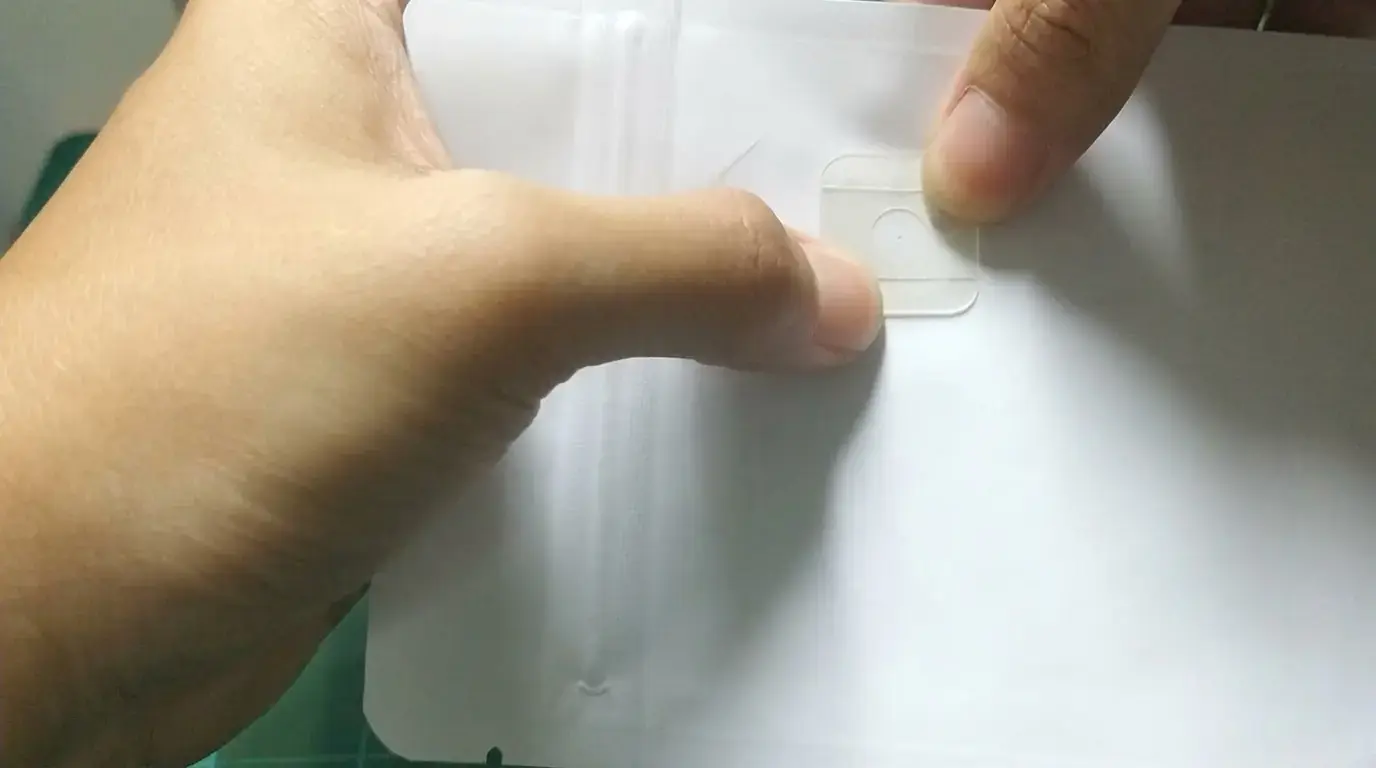
A stick-on coffee valve is applied to the outside surface of the coffee bag. The package has a vent opening, and the valve is positioned over the opening and attached to the package surface.
This degassing valve sticker configuration can be suitable for existing bag formats and certain manual or semi-automatic workflows. Its main installation controls are valve position, surface condition, and attachment quality.
How a Built-In Coffee Valve Works
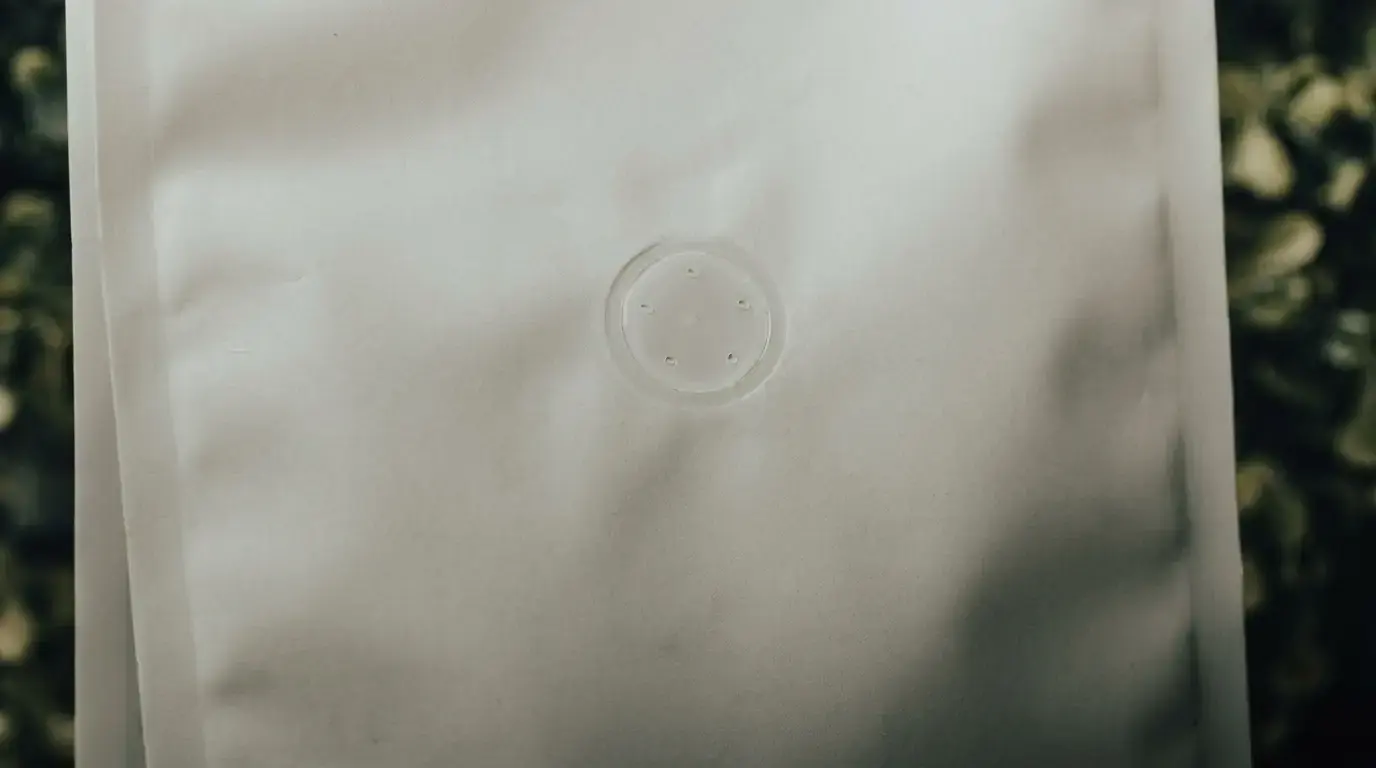
A built-in coffee valve is incorporated into the pouch during bag manufacturing or converting. Its position and attachment are established during package production rather than added separately afterward.
Why “Stick-On” Does Not Mean Lower Performance
Both configurations can provide one-way degassing. Terms such as freshness valve, coffee aroma valve, and valve for coffee bags describe the application or function, while “stick-on” and “built-in” describe the installation approach.
The installation method therefore does not, by itself, determine valve quality. The package and production process also need to be considered.
How Does Installation Differ Between Stick-On and Built-In Coffee Valves?
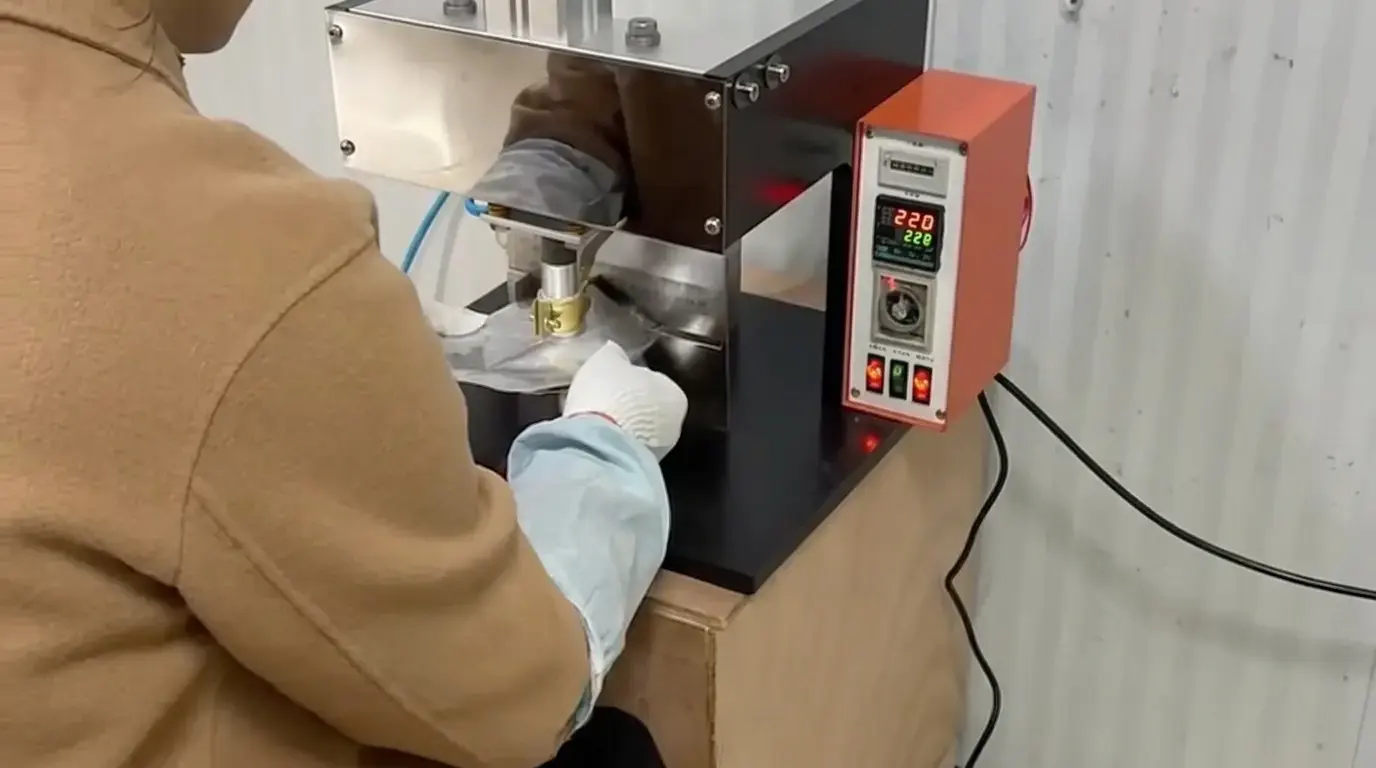
Stick-On Coffee Valve Installation
The basic process involves preparing the vent opening, positioning the valve over it, and attaching it to the package surface.
The main controls are:
- Correct vent-hole position
- Accurate valve alignment
- Suitable and clean package surface
- Consistent attachment
- Protection during subsequent handling
Because the valve is applied separately, application becomes an additional production step. This can be useful when a manufacturer needs to add a valve to an existing or established bag format.
Built-In Coffee Valve Installation
A built-in valve is incorporated during pouch manufacturing or converting. Its position and attachment are established before the finished bag reaches the filling stage.
This removes a separate valve-application step, but makes valve integration part of the pouch production process. Placement, attachment, and compatibility with the film structure therefore become important process controls.
Installation Changes the Main Risk Point
The distinction is straightforward:
- Stick-on: application, adhesion, and alignment
- Built-in: integration, placement, and pouch production consistency
The two configurations therefore require different quality-control priorities.
What Are the Common Failure Modes of Stick-On Coffee Valves?
A stick-on valve can fail because of the valve mechanism, the attachment interface, or the way it is installed.
Edge Lift or Poor Adhesion
Poor attachment between the valve and package surface can cause the valve to lift from the bag. Surface contamination, unsuitable package conditions, or inconsistent application can contribute to this problem.
Leakage Around the Valve
The valve mechanism may function correctly while the surrounding interface leaks. The adhesive or attachment interface therefore needs to remain compatible with the package surface during handling and storage.
Incorrect Hole or Valve Position
The vent opening and valve need to be properly aligned. Incorrect positioning can interfere with the intended gas path and create inconsistent results.
Mechanical Damage
Filling, handling, transportation, or other packaging operations can damage an exposed valve. Damage may affect its ability to vent or reseal.
For troubleshooting, examine the system in this order:
Valve mechanism → attachment/interface → vent opening → package film → application process
The important point is that degassing valve sticker failures are not necessarily caused by the valve mechanism itself. The valve-package interface is another critical control point.
What Are the Common Failure Modes of Built-In Coffee Valves?
Integrating a valve into the pouch does not eliminate failure risks. Instead, some controls move into the pouch manufacturing process.
Inconsistent Valve Installation
Variation in valve position or attachment can affect finished-package consistency. Production control is therefore important when the valve is integrated into the pouch.
Valve-to-Film Attachment Problems
The connection between the valve and pouch structure needs to remain reliable. Material compatibility and production conditions can affect the attachment.
Valve Mechanism Problems
Built-in valves can experience mechanism-related problems, including failure to open as intended or inconsistent resealing.
Placement Conflicts
Valve placement needs to work with pouch forming, filling, sealing, and handling. A suitable built-in coffee valve can still create problems if its integration into the package is poorly controlled.
The diagnostic focus is therefore:
Valve mechanism → valve/film attachment → placement → pouch production process
This is different from the main control path for a stick-on valve.
Does a Stick-On or Built-In Valve Provide Better Performance?
Neither configuration should be treated as universally superior. The more useful comparison is how each performs within the intended packaging system.
One-Way Degassing
Both configurations can be designed to provide one-way CO₂ release. The relevant question is whether the valve vents consistently after installation in the actual coffee package.
Air Blocking and Resealing
A coffee one-way valve needs to allow gas to escape while limiting unwanted air ingress. Problems can originate from either the valve mechanism or the connection between the valve and package.
Finished-Package Integrity
For this reason, valve performance should be considered together with the package rather than evaluated only as an isolated component.
| Performance Factor | Stick-On | Built-In |
|---|---|---|
| One-way degassing | Can support | Can support |
| Main control point | Application | Integration |
| Interface risk | Adhesive/package surface | Valve/film attachment |
| Package compatibility | Important | Important |
| Finished-package testing | Required | Required |
The practical conclusion is that installation method changes the risk profile, but does not by itself determine performance.
Stick-On vs Built-In Coffee Valves: Which Is Better for Different Production Setups?
The appropriate valve for coffee bags depends largely on how the bags are produced and filled.
| Production Consideration | Stick-On | Built-In |
|---|---|---|
| Existing bags | More adaptable | Usually requires compatible production |
| Manual application | More suitable | Less relevant |
| Semi-automatic workflow | Possible | Possible |
| Integrated pouch production | Separate application step | Naturally integrated |
| Main risk | Adhesion/application | Integration/placement |
| Main validation focus | Bonding + alignment | Attachment + pouch production |
When Does a Stick-On Coffee Valve Make More Sense?
A stick-on configuration can be practical when:
- Existing bag formats need to be maintained
- Valve application is manual or semi-automatic
- Production formats vary
- A separate valve-application step is acceptable
It can provide flexibility where changing the pouch manufacturing process would be unnecessary.
When Does a Built-In Coffee Valve Make More Sense?
A built-in configuration can be suitable when valve integration is planned from the beginning of pouch development and can be incorporated into the converting process.
It is particularly relevant when consistent valve placement and integrated production are important requirements.
Why Package and Process Should Drive the Decision
The choice should not be based on the assumption that built-in means higher quality or stick-on means lower quality.
Instead, buyers should evaluate:
Bag structure + valve compatibility + installation process + production control
This gives a more practical basis for selecting a coffee package valve.
How Should Coffee Valve Performance Be Validated?
Validation should focus on the valve after it has been integrated into the intended package.
Check Installation Integrity
For stick-on valves, check:
- Valve position
- Alignment with the vent opening
- Attachment quality
- Package surface compatibility
- Visible defects or edge lifting
For built-in valves, focus on placement, attachment to the pouch structure, and production consistency.
Test One-Way Venting
Confirm that the valve allows gas to escape as intended and that results remain consistent across samples.
Testing installed valves is more representative than evaluating loose components alone.
Check Leakage and Resealing
Evaluate both the valve mechanism and the valve-package interface. A component can pass an individual inspection while the finished package still develops a leakage problem.
Test the Finished Coffee Package
Where appropriate, use the intended bag structure and production process. Testing can include the conditions the package is expected to encounter during filling, handling, storage, and transportation.
The goal is to verify the complete valve-package system, rather than repeat a component-level performance check.
What Should You Ask a One-Way Valve Supplier Before Ordering?
For bulk buyers, choosing a one-way valve supplier in China is not simply a matter of comparing unit prices. The supplier should provide information that supports compatibility and production validation.
Confirm Valve Specifications
Ask about:
- Valve construction
- Available materials
- One-way venting characteristics
- Resealing behavior
- Available configurations
The specification should be matched to the intended package rather than treated as a universal requirement.
Confirm the Installation Method
Clarify whether the valve is designed for:
- Stick-on application
- Built-in integration
- Manual application
- Semi-automatic application
- Integrated pouch production
Also confirm any requirements for the vent opening and package surface.
Confirm Package Compatibility
Provide information about the intended coffee bag structure, film surface, sealing process, and production method. This allows the supplier to evaluate the valve as part of the actual packaging system.
Request Samples Before Bulk Production
Before placing a large order, test samples using the actual bag structure and intended installation process. Check installation consistency, venting, resealing, leakage, and finished-package integrity.
Evaluate the Supplier Beyond Unit Price
For buyers sourcing from a coffee valve manufacturer, manufacturing capability matters alongside the component specification.
Sanrun provides coffee valves and packaging components with OEM/ODM support for buyers requiring customized solutions. Its manufacturing and quality-control capabilities can be evaluated together with the required valve configuration and package requirements.
A capable custom coffee valve manufacturer should be able to discuss the component, application method, package compatibility, quality control, and bulk-production requirements—not simply provide a quotation.
Conclusion
The choice between stick-on and built-in should follow the packaging process.
Choose a stick-on coffee valve when flexibility with existing bag formats and separate valve application are important. Choose a built-in configuration when valve integration can be planned as part of pouch production and consistent placement is a priority.
The decision can be reduced to four questions:
- What bag structure will be used?
- When and how will the valve be installed?
- Where is the main production risk?
- How will the finished package be validated?
For both configurations, the objective is the same: establish a reliable one-way degassing solution that works within the actual coffee packaging process.
About Sanrun – Your Reliable Bulk Coffee Valve Manufacturer
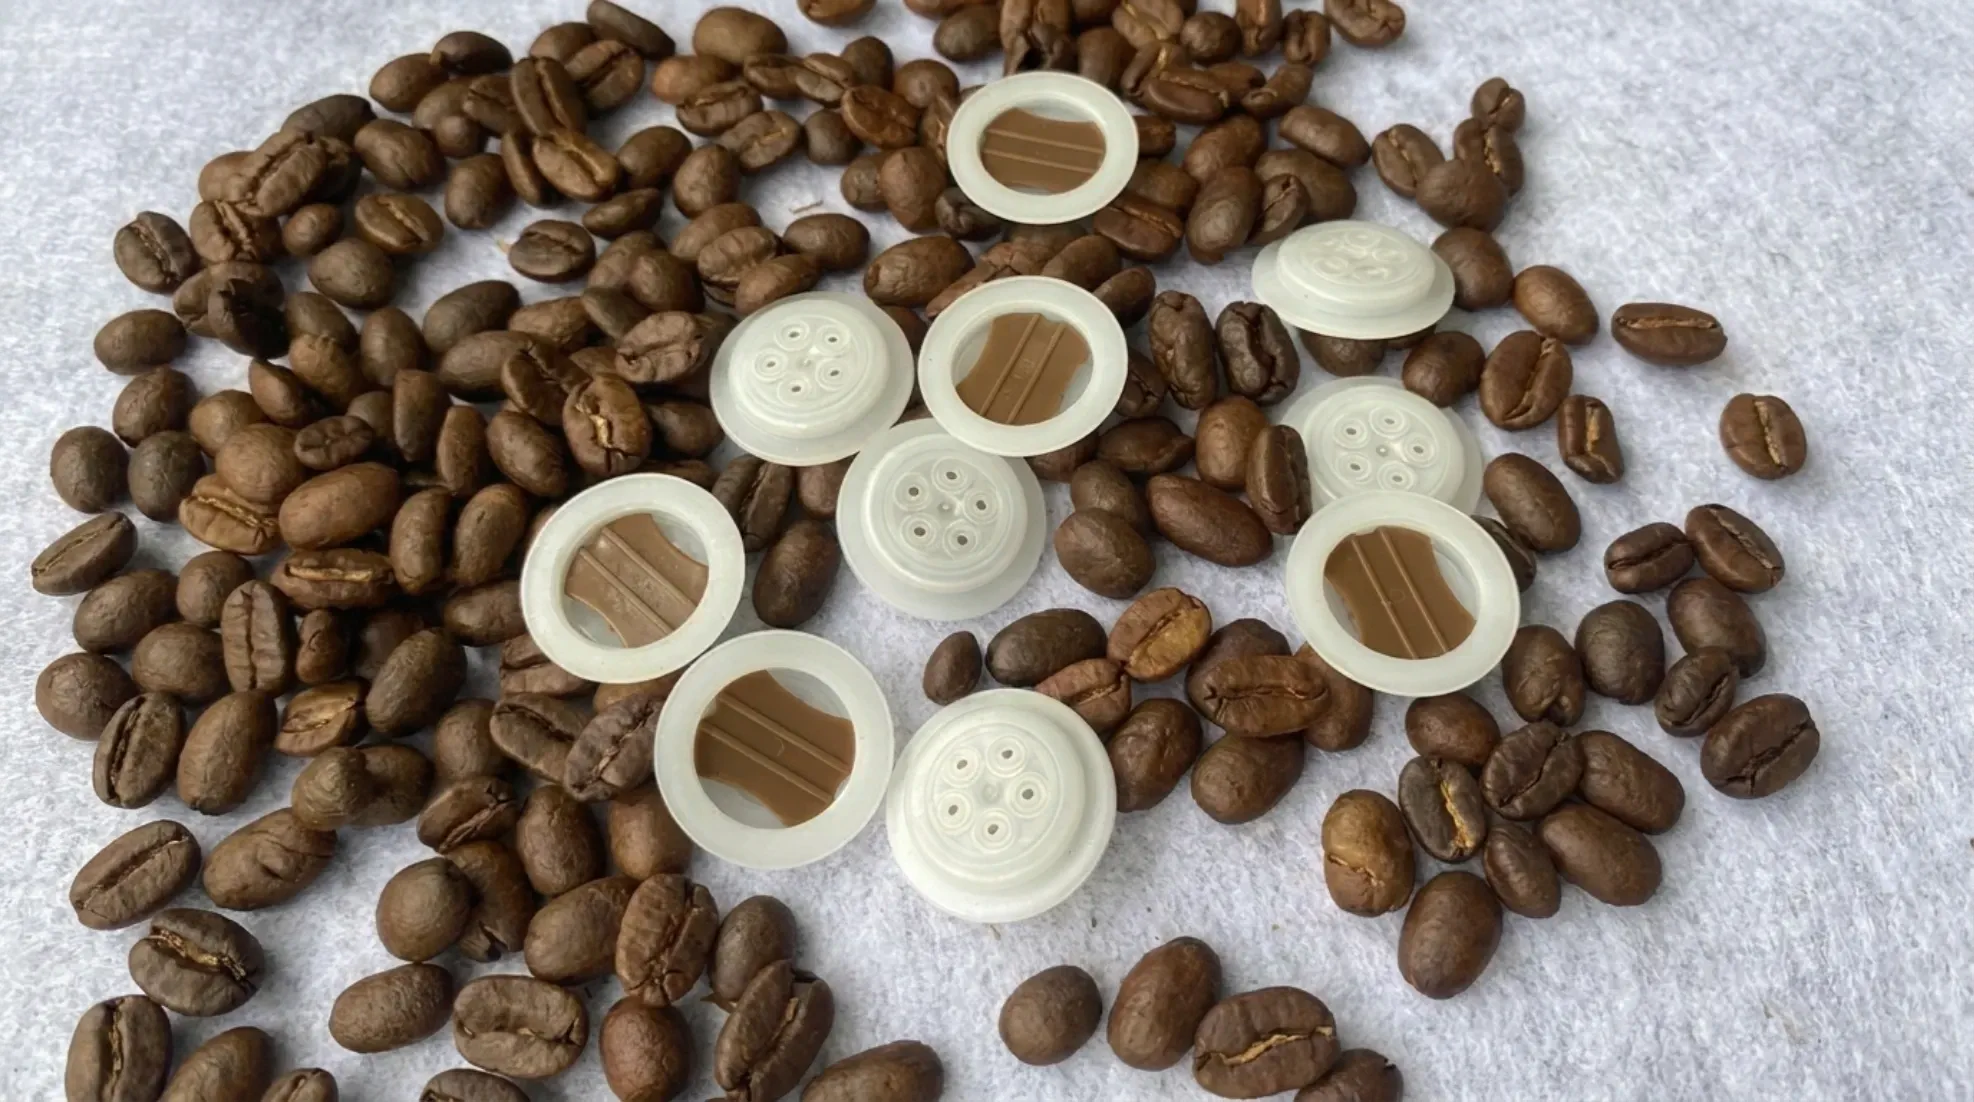

Sanrun is a professional coffee valve manufacturer serving coffee brands, flexible packaging manufacturers, wholesalers, and distributors worldwide. With a customer-focused approach, Sanrun provides OEM and ODM customization for one-way degassing coffee valves, helping customers match valve configurations with their bag structures, installation methods, and production processes.
Our products are manufactured under strict quality control, with relevant certifications supporting international packaging requirements. From valve selection and sample validation to customized bulk production, Sanrun works closely with B2B customers to develop reliable one-way degassing solutions tailored to their packaging needs.